

 Español
 Francés
 Português
 Italiano
 Türk
 العربية
 Русский
 한국어
 日本語


Solar Thermal Absorber Coating
D-DOS (Black Film) Coating
· Solar Absorptance: α = 94% ±2% (@AM1.5)
· Outstanding durability against weathering and salt spray, enabling wider application adaptability
· Cost-effective performance with reliable quality using D-DOS coating technology
I. Product Introduction
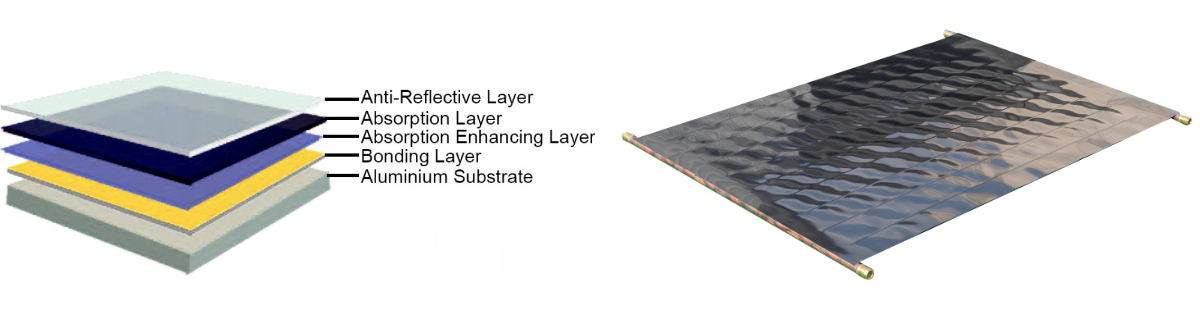
Black Solar Coating (solar black film), also known as nano black chromium solar spectral high-selectivity absorption coating, is a solar spectral selective absorption coating and one of the core materials in the field of solar thermal utilization. This coating is deposited on the surface of a metal substrate using advanced vacuum magnetron sputtering (PVD) technology and is used to efficiently collect solar energy and convert it into thermal energy.
In the core structure of flat solar collectors, the film layer is the "soul component" that determines the efficiency of photothermal conversion. It is like a precise optical filter, converting solar radiation into thermal energy while minimizing heat loss. Black Solar Coating has an extremely high solar absorption rate in the main energy range of solar radiation (0.25 - 2.5 μm) and maintains a low thermal emission rate in the infrared band (> 2.5 μm), achieving ideal spectral selectivity of high absorption and low emission.
Our company's Black Solar Coating is an upgraded version of the original black titanium film, featuring high photothermal conversion efficiency, long service life, and low overall cost. In 2017, our company successfully developed the second-generation black film technology, reducing manufacturing costs by 30% while maintaining excellent optical performance. Currently, it occupies 60% of the black film market in China. The film layer is based on an aluminum substrate with a thickness of 0.3 - 0.4 mm (customizable), and the surface coating thickness is only 150 nanometers, yet it meticulously constructs a 7-layer structure including a bonding layer, a blocking layer, and an infrared reflection layer. The optimized high-performance black film has a solar absorption rate (α) of up to 94% - 96% ± 2% (AM1.5) and an infrared emissivity (ε) of 6% - 8% ± 2% (@80°C). As the only enterprise in the world that simultaneously masters the core production technologies of blue and black films, we provide customers with a one-stop solution for high-selectivity solar absorption coatings.

II. Product Parameters
Parameter Item Technical Indicators
Product Name High Selective Solar Absorber – Black Solar Coating
Model | Base Material | Coaing Type | Absorption ratio (%) | Emission ratio (%) |
thickness:0.3/0.4mm width:750/950/1200/1250mm Customizable | AI | Black coating film | 94±2% | 12+2% |
thickness:0.3/0.4mm width:750/950/1200/1250mm Customizable | AI | Blue coating film | 95+2% | 5+2% |
III. Product Advantages
1. High absorption, low emission, excellent photothermal conversion efficiency
The solar absorption rate of Black Solar Coating is up to 94% - 96% above, and the thermal emission rate is low to 6% - 8% below. Compared with the first-generation black film product, the performance has improved by more than 20%. In the application of flat solar collectors, it can maximize the conversion of solar energy into thermal energy, significantly improving the collection efficiency.
2. Significant cost advantages and outstanding cost performance
As an upgraded product of the second-generation black film technology, our black film ensures excellent optical performance while reducing manufacturing costs by 30%. Compared to blue film, the black film has higher cost performance, especially suitable for large-scale promotion scenarios. Currently, our black film products have occupied 60% of the black film market in China.
3. Excellent spectral selectivity
The black film, as a selective absorption coating for solar radiation, has high absorption characteristics in the main energy range of solar radiation, while maintaining a low emissivity in the infrared band, achieving an ideal spectral selective absorption effect.
4. Outstanding weather resistance and long lifespan
The membrane layer of the flat solar collector needs to face harsh environments such as ultraviolet rays, salt fog, temperature differences, and sandstorms. Our black film enhances the reliability of the membrane layer through technologies such as anti-ultraviolet aging, salt fog corrosion resistance, and thermal shock resistance. According to authoritative tests, the product has a lifespan of up to 25 years.
5. Advanced technology, stable quality
We adopt a fully automatic magnetron sputtering high-weather-resistant selective absorption coating production line to achieve large-scale, high-efficiency, and continuous production. The second-generation membrane layer production line effectively solves the defects of the first-generation product, such as poor performance stability, residual film layer on the back affecting welding, poor uniformity of the membrane layer, and unstable optical performance.
6. Compatible with multiple substrates
The product can be plated on various metal substrates such as aluminum plates, copper plates, and copper strips. The strip type and whole plate type can be customized to meet the needs of different application scenarios.
Four. Factory advantages - Dual-line production capacity of blue film and black film
As a professional manufacturer in the field of selective absorption coatings for solar energy, our company has the industry-leading fully automatic magnetron sputtering high-weather-resistant selective absorption coating production line. We are the only supplier in the world that can simultaneously produce nano black chromium solar spectral high-selectivity absorption coatings (black film) and vacuum magnetron sputtering (PVD) solar spectral high-selectivity absorption coatings (blue film).
1. Black film production line: The second-generation black film technology was developed in 2017, reducing manufacturing costs by 30%, and currently occupies 60% of the black film market. The absorption rate of black film products is ≥ 94%, the emissivity is ≤ 8%, and the performance has improved by more than 20% compared to the first generation. It is suitable for large-scale application scenarios with high cost performance requirements.
2. Blue film production line: The Bonding blue film technology was successfully developed in 2011 and obtained a national invention patent. The absorption rate of blue film products is ≥ 95%, the emissivity is ≤ 5%, and it is suitable for the high-end flat collector market.
3. Full-chain layout: From equipment research and development to membrane layer production, our company has complete independent intellectual property rights and core technologies, and the related equipment research and development has gone through three generations of iterations.
4. Collaboration with universities and research institutions: The company has deep cooperation with the Institute of Semiconductors of the Chinese Academy of Sciences, Tsinghua University, and Shandong University, forming an "industry, academia, research" combined industrial layout.
5. Production capacity: Annual production of 5 million square meters of nano black chromium solar high-selectivity absorption coatings, ranking among the top in the world.
Whether it is the blue film that pursues ultimate performance or the black film that balances performance and cost, we can provide customers with the optimal solar selective absorption coating solution.
Five. Packaging and transportation
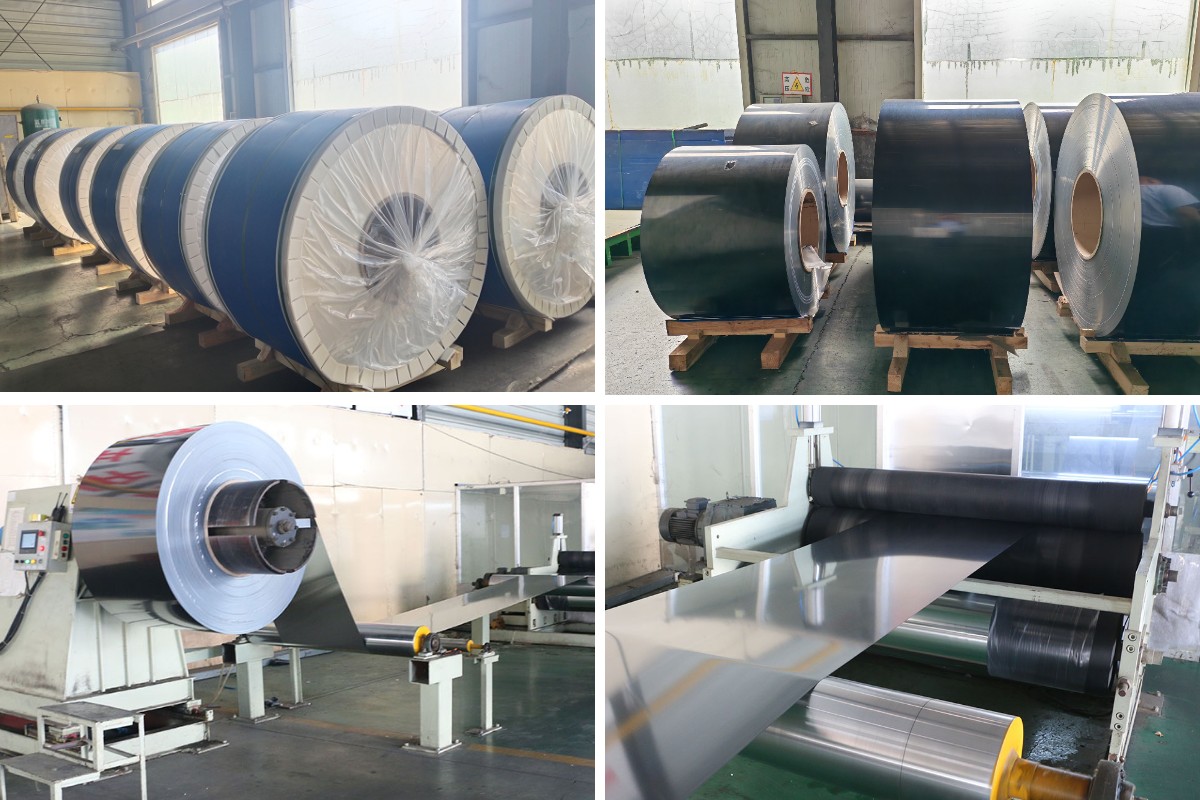
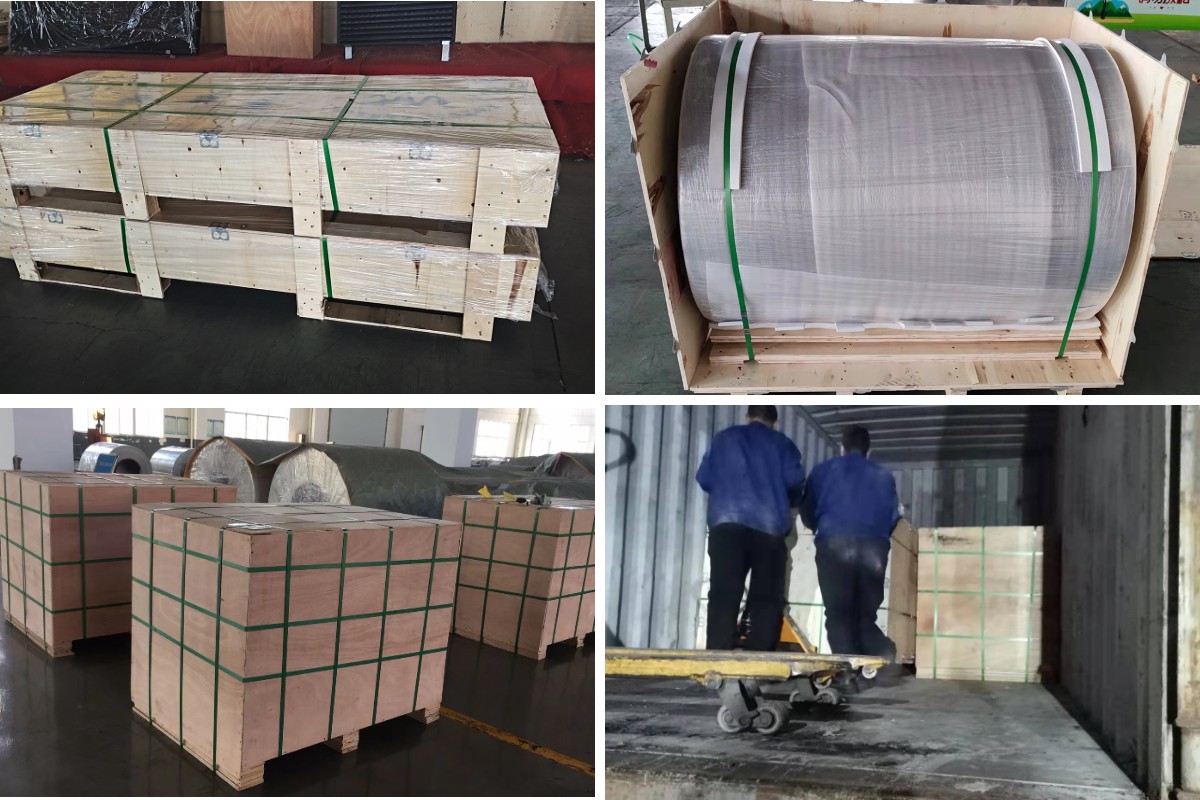
Packaging method: The membrane layer products are packaged with moisture-proof and shock-proof packaging. The inner layer is covered with PE protective film, and the outer layer is packaged with high-strength corrugated cardboard or wooden boxes.
1. Each roll of product is independently packaged, with clear labels, including product specifications, batch number, production date, etc.
2. Customized packaging solutions can be provided according to customer requirements.
Transportation method:
1. Support various transportation methods including sea, air and land.
2. During the product transportation process, it is protected from moisture, impact and pressure to ensure the product is delivered intact.
3. We can deliver the products in batches according to customer requirements, flexibly meeting the needs of different orders.
4. We provide one-stop logistics services including export customs declaration and clearance.
VI. Application fields
Black Solar Coating, as the core material of solar thermal conversion collectors, is widely used in the following fields:
1. Flat solar collectors - solar hot water systems
The black film is an important heat-absorbing material for efficient flat-type solar collectors and is widely used in household and commercial solar hot water supply systems.
2. Solar heating systems
Suitable for building-integrated solar heating, effectively reducing building energy consumption.
3. Solar thermal power generation
Suitable for low and medium temperature solar thermal power generation systems' heat collection components.
4. Desalination of seawater
As the core material of solar thermal conversion, it is applied in solar seawater desalination systems.
5. Dual-source heat pump systems
Suitable for solar and air-source dual-source heat pump systems, achieving multi-energy complementarity.
6. Industrial heat and building energy conservation
Widely used in clean energy fields such as industrial process heat and building energy conservation.

Contact us immediately to obtain product quotations and technical solutions!
Whether you need high-selectivity black solar film or high-selectivity blue solar film, whether you are a manufacturer of flat collectors, a solar hot water project provider or a new energy project developer, we are willing to provide professional product consultation and technical support for you.


